
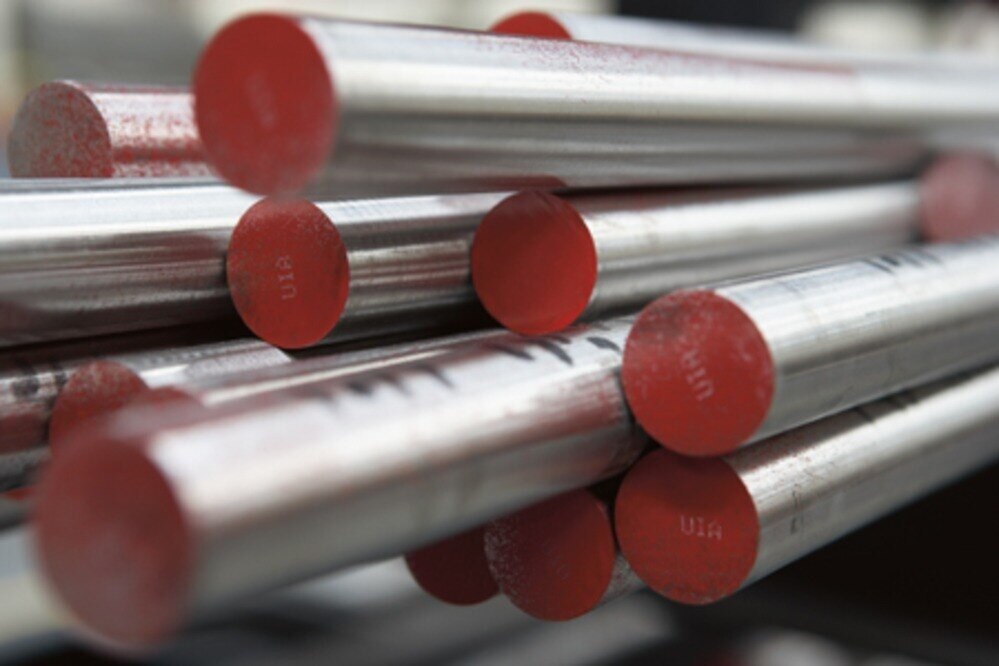
Choosing SA 516 Gr 70 is not a matter of matching a grade name to a vessel sketch. You need to connect the plate’s strength, toughness, dimensions, heat-treatment condition and traceability to the equipment’s design code, fabrication route and service conditions, then verify those details before cutting begins.
Key takeaways
- Use SA 516 Gr 70 for welded pressure boundaries, shells, heads and formed sections.
- Specify thickness, delivery condition, test requirements and certificate details on the purchase order.
- Compare Grade 60, Grade 70 and SA 515 against design strength and temperature needs.
- Inspect plate markings, dimensions, documents and traceability before cutting begins.
Where SA 516 Gr 70 Plate Fits in Industrial Equipment
SA 516 Gr 70 fits the pressure boundary of welded industrial equipment: the shells, heads and formed sections that contain internal pressure. Its controlled pressure-vessel chemistry, strength, toughness and weldability make it suitable for sa 516 gr 70 industrial applications, rather than treating it as ordinary structural plate.
| Component | Where the plate is used | Why it fits |
|---|---|---|
| Air receivers | Cylindrical shells and dished heads | Weldable, pressure-rated plate for repeated compressed-air service |
| Separators and flash vessels | Shells, heads and nozzles | Suitable for welded containment under process pressure and temperature |
| Heat exchangers | Shell courses and channel shells | Supports fabricated pressure boundaries around fluids and vapour |
| Storage vessels and process vessels | Shells, roofs designed for pressure, and heads | Provides predictable properties for calculated wall thickness |
| Boiler drums | Drum shells and formed heads | Intended for welded boiler and pressure-vessel construction |
| Other equipment | Reactors, accumulators and filter housings | Available in plate thicknesses suited to engineered fabrication |
SA 516 plate for manufacturing is selected for the pressure boundary; supports, platforms, ladders and base frames can use carbon structural steel or other specified materials because they do not contain pressure.
Grade 70 alone does not approve a finished vessel. The governing construction code, design pressure, design temperature, calculated thickness, corrosion allowance, impact requirements and qualified weld procedures decide acceptance.
Do not substitute IS 2062 or another structural grade because its strength figures look similar. Pressure service also depends on toughness, weldability, heat treatment, inspection traceability and any specified through-thickness quality.
How Chennai Fabricators Turn Plate into Pressure Equipment
A fabricator turns SA 516 Gr 70 plate for manufacturing into a pressure boundary through controlled cutting, forming, welding and inspection; every stage can affect suitability.
1. Incoming inspection checks the purchase specification, mill certificate, thickness, dimensions, surface condition and heat number. In Chennai, keep plates raised, dry and separated with water-shedding supports during monsoon or coastal storage.
2. Inspect oxidation closely. Blasting or repainting removes loose rust, not pitting that has reduced thickness; reject or assess affected plate against the permitted minimum.
3. Mark each plate before CNC or profile cutting, then transfer the heat number to every shell course, head, nozzle and other pressure-boundary part. Retain the original identification record after nesting or shearing.
4. Edge preparation removes cut-affected material where the approved procedure requires it. Thermal cutting can alter the local condition, so bevel quality, hardness and any required examination must follow the qualified procedure.
5. Roll the plate into shells and form or dish heads within the approved forming limits. Excessive cold work, unsuitable tooling or unapproved heating can change dimensions and material condition.
6. Fit-up controls gap, alignment, roundness and restraint before welding. The welding procedure must address thickness, carbon equivalent, restraint, hydrogen control, consumables, preheat and interpass temperature; weldable does not mean preheat can be skipped.
7. Complete welding, then apply stress relief or code-required post-weld heat treatment. Later heat treatment can alter local properties, so the approved vessel procedure must cover it.
8. Machine faces, nozzles and openings before dimensional inspection, weld examination and hydrostatic testing confirm the finished equipment’s integrity. For SA 516 Gr 70 plate for uses in Chennai, release the vessel only when records, dimensions and test results agree.
How to Choose Grade 70, Grade 60 or SA 515
Choose SA 516 Grade 70 when the vessel thickness calculation, design margin and governing code benefit from its higher minimum strength, and the forming and welding route can accommodate it. Do not choose it simply because 70 is the larger number.
| Grade | Minimum yield strength | Tensile strength range | Selection implication |
|---|---|---|---|
| SA 516 Grade 60 | 32 ksi (220 MPa) | 60–80 ksi (415–550 MPa) | Compare where lower strength meets the calculated design requirement and forming or welding demands favour it |
| SA 516 Grade 70 | 38 ksi (260 MPa) | 70–90 ksi (485–620 MPa) | Offers higher minimum strength, but does not alone prove better vessel suitability |
The final choice must follow the vessel thickness calculation, forming route, design margin, code rules and required toughness. Higher strength does not automatically mean easier rolling, simpler weld-procedure controls or acceptable service at the design temperature. These factors govern SA 516 Gr 70 industrial applications as much as tensile values do.
SA 516 is associated with welded pressure-vessel plate for lower or moderate temperatures with controlled toughness. Compare SA 515 when boiler or pressure-vessel service involves higher temperatures under the applicable specification and design code. Neither product name replaces a design review.
For sub-ambient metal temperatures, put the specified Charpy impact-test temperature and absorbed-energy result in the purchase documents. For sour service, add hardness limits, environmental qualification and cracking controls; Grade 70 alone does not certify sulfide-stress-cracking resistance.
What to Put on the Purchase Order and Material Certificate
A plate stamped ASTM A516 Grade 70 is not automatically code-acceptable SA-516 material. “SA” identifies the ASME Section II material listing; require the correct ASME/ASTM edition, purchase specification and certificate before releasing it for vessel fabrication.
Write these items on the purchase order:
- SA-516 or ASTM A516/A516M, applicable edition, Grade 70, thickness, width and length
- Delivery condition, including normalized or normalized-and-tempered condition when required
- Design or test temperature and the specified Charpy impact-test temperature and energy
- Ultrasonic testing to the named standard, where specified
- Thickness tolerance, surface-acceptance criteria and every supplementary project requirement
- Independent testing when required by the construction code or project specification
Do not accept “Grade 70” as proof of normalizing; the heat-treatment condition must be stated.
| Document | What to verify | Why it matters |
|---|---|---|
| EN 10204 Type 3.1 inspection certificate | Purchaser-facing inspection results, not a generic certificate of conformity | Connects ordered requirements to tested material |
| Plate marking | Heat number and plate number, or retained marking after cutting | Preserves identity through fabrication |
| Mill test results | Chemistry, tensile strength, yield strength, elongation, dimensions, heat treatment and impact temperature/results when ordered | Shows whether the delivered plate matches the order |
Match both numbers on the plate to the mill certificate. For SA 516 Gr 70 plate for uses in Chennai, retain photographs or transferred markings before profiling. A certificate without traceable identity, or a plate without agreed thickness tolerance and surface acceptance, is not complete evidence that the vessel requires it.
How to Evaluate a Chennai Supplier Before the Plate Is Cut
Price is only the starting filter. A boiler plate supplier in Chennai must match the vessel code, purchase order and inspection plan with the actual plate offered, not merely quote SA 516 Grade 70.
Ask for:
- The original mill certificate, preferably EN 10204 Type 3.1, showing heat number, plate number, chemistry, tensile and yield results, elongation, dimensions and heat-treatment condition.
- Continuous heat-number identification after shearing or profiling, with a marking-transfer plan and photographs or records of the original plate marking before division.
- Dimensional inspection, surface-condition records, agreed Charpy temperature and absorbed-energy results, and ultrasonic-testing results where specified. Arrange independent testing when the code or project inspector requires it.
Stock status can decide whether the job starts on time.
| Plate issue | Consequence |
|---|---|
| Correct thickness, wrong width or length | Extra profiling, unusable nesting or rework |
| Correct grade, wrong heat-treatment condition | Rejection against the purchase order or code |
| No required impact qualification | Material cannot serve the specified low-temperature duty |
Inspect the surface for pitting. Blasting or repainting removes rust but does not restore metal lost to corrosion. Require dry, raised storage with water-shedding separation during Chennai monsoon or coastal exposure.
Steel Mart can be a procurement resource when it supplies tested, certified plate with traceable documents; verify every claim against your requirements for SA 516 Gr 70 plate for uses in Chennai.
Do not release plate to rolling or welding until specification, certificate, heat identity, dimensions and required test results agree.
Related product
 | BQ and Wear Resistant Plates SA 516 Gr 60-70 Boiler Quality Plate SA 516 Grade 60 / Grade 70 Boiler Quality Plate is a pressure vessel quality carbon steel plate designed for medium to low-temperature service. View product → |
Frequently asked questions
Where does SA 516 Gr 70 plate fit in industrial equipment?
It fits welded pressure boundaries, including vessel shells, heads and formed sections that contain internal pressure. It is used in equipment such as process vessels, boilers, storage tanks and heat-exchanger components when the design specification calls for SA 516 Gr 70.
How do Chennai fabricators turn SA 516 Gr 70 plate into pressure equipment?
They inspect and identify the plate, cut it, bevel edges, roll or press-form sections, fit and weld the parts, then complete heat treatment, non-destructive testing and pressure testing required by the design code.
How do Grade 70, Grade 60 and SA 515 differ?
SA 516 Gr 70 provides higher minimum tensile and yield strength than Grade 60 within the standard, while SA 515 is intended for pressure-vessel plates for moderate and higher-temperature service. Select among them using the design code, temperature, thickness, toughness and welding requirements.
What should you put on the purchase order and material certificate?
State SA 516 Grade 70, plate thickness and dimensions, quantity, delivery condition, heat-treatment requirement, impact-test temperature, supplementary tests, applicable edition of the standard and certificate type. Check the material certificate for heat number, chemistry, tensile results, yield strength, elongation, impact results when specified and traceability.
How can you evaluate a Chennai supplier before the plate is cut?
Verify the supplier’s test certificate against the plate heat number and markings, measure thickness and dimensions, inspect for laminations or damaging surface defects, confirm delivery condition and review whether the supplier can provide the required inspection and traceability records.